
Learn how #100 and #101 behave in Fanuc Macro B, why globals pass into subprograms, and how to safely use #100–#149 with Renishaw probing cycles. Do #100 and #101 Pass Into a Subprogram? Yes — Here’s the Clean Truth If you set #100 and #101 before c...
Read More
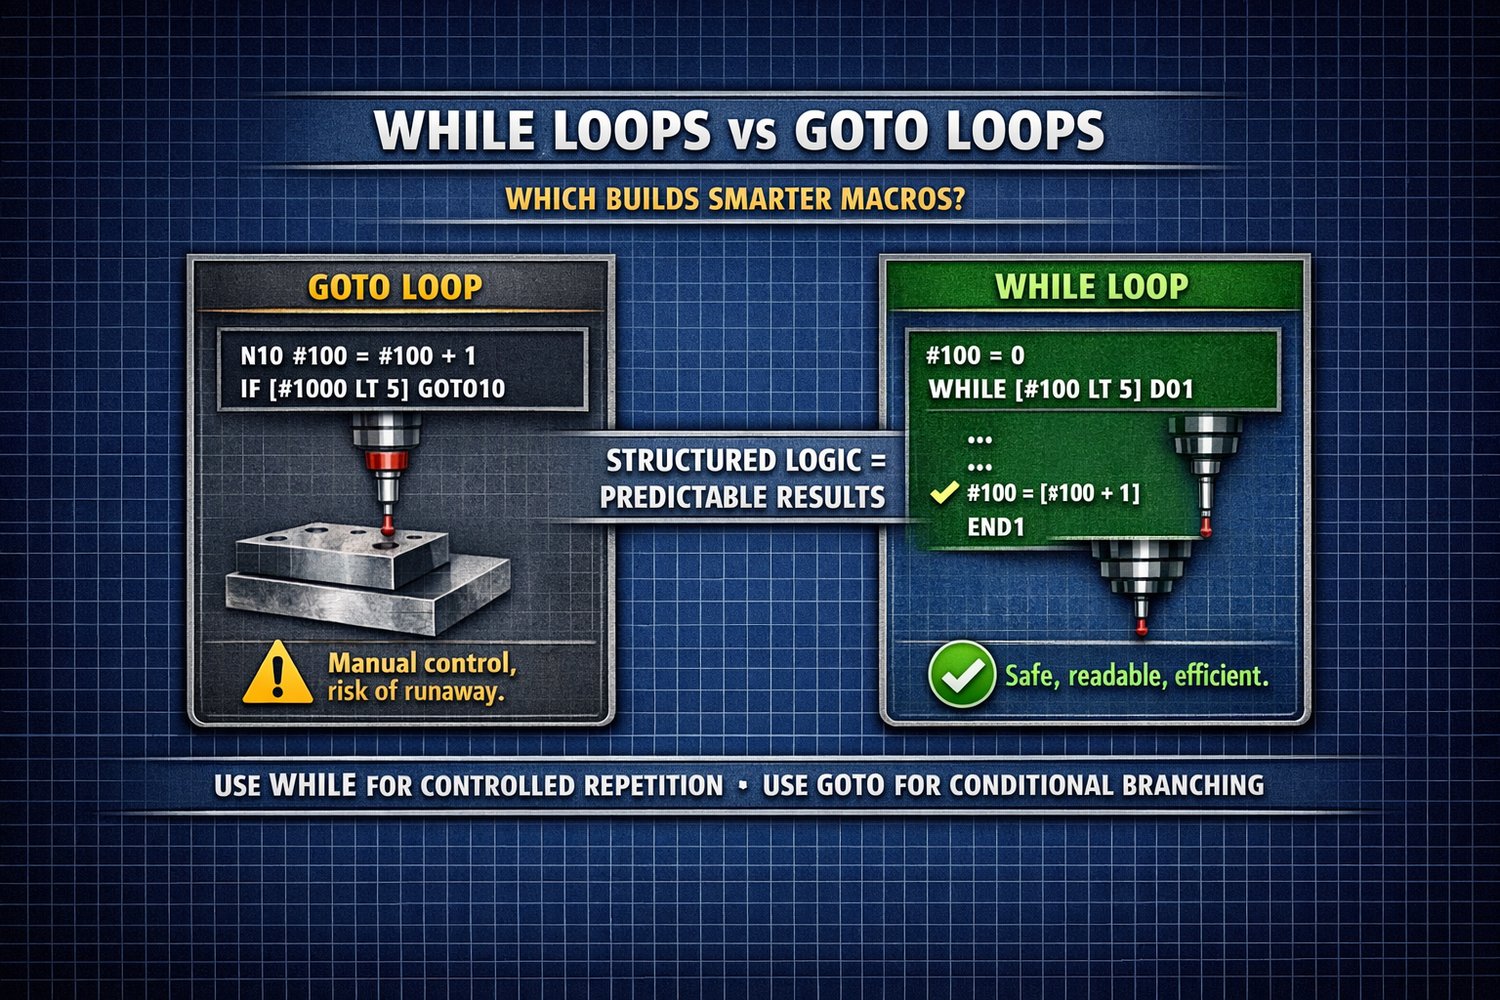
If you’ve ever wondered whether WHILE loops or GOTO loops make better Fanuc Macro B programs, the answer comes down to structure, safety, and predictability. WHILE loops give you controlled repetition, while GOTO loops handle conditional branching —...
Read More
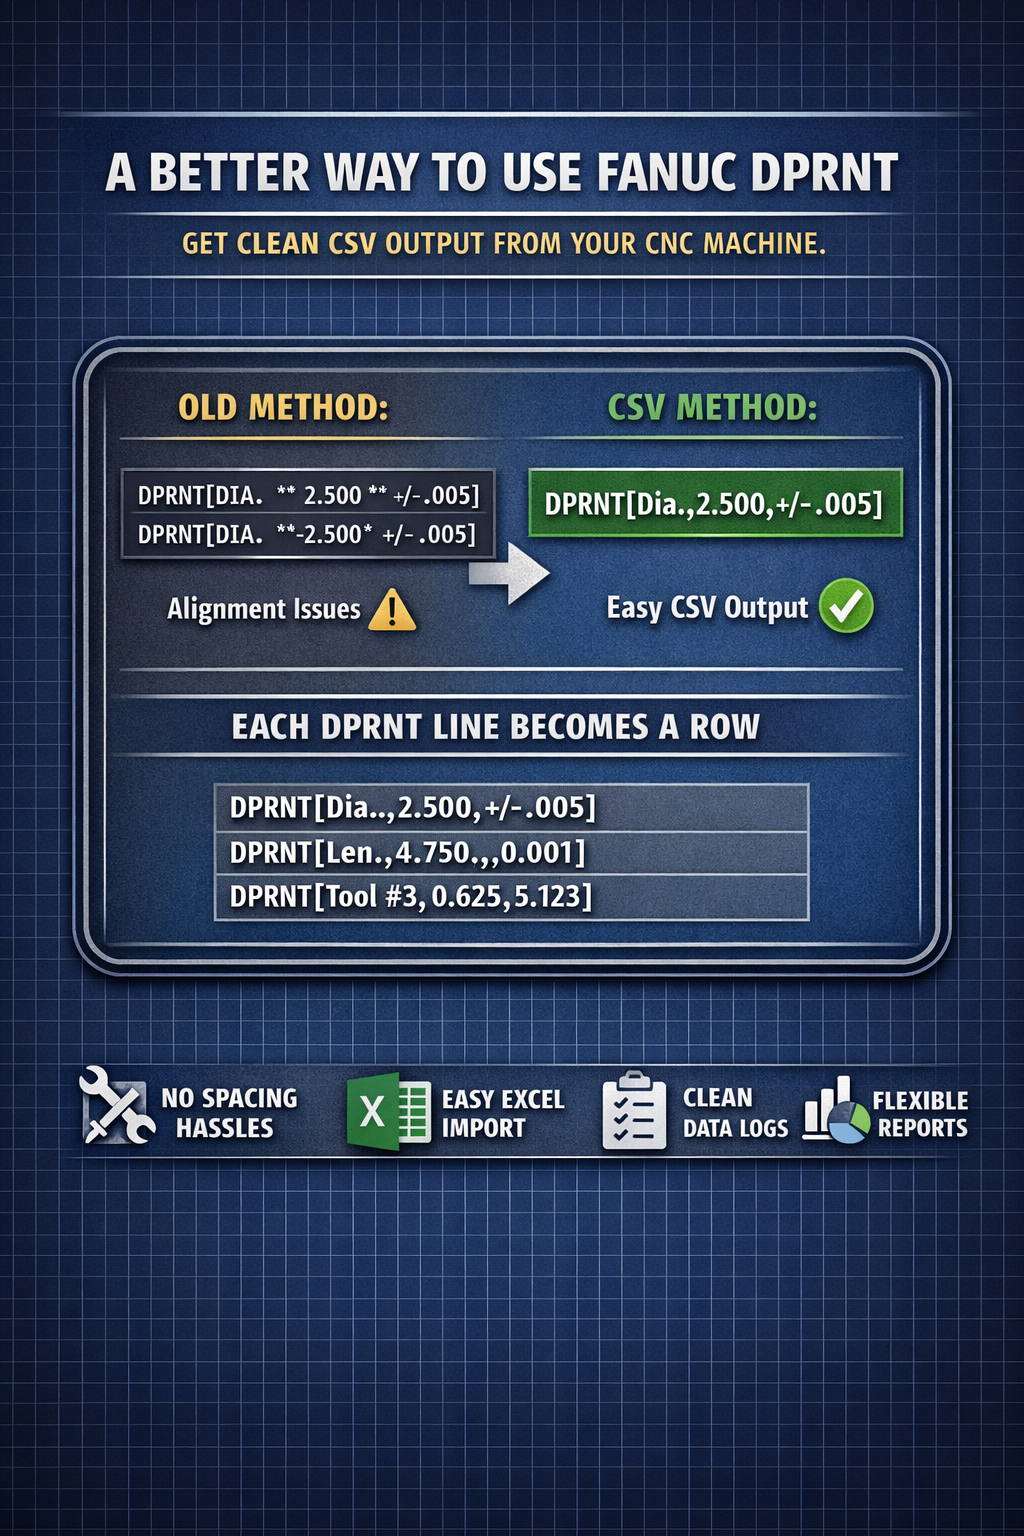
Learn a cleaner, easier way to use Fanuc DPRNT by exporting CSV‑ready data for Excel or Google Sheets. No spacing issues, no alignment problems — just clean CNC reporting. If you’ve spent any time with Fanuc’s DPRNT feature, you already know one th...
Read More
Twenty years ago, machining looked very different. Most shops were running older controls, handwritten notes were the norm, and a lot of tribal knowledge lived in the heads of a few seasoned operators. If you wanted to learn something, you stood be...
Read More